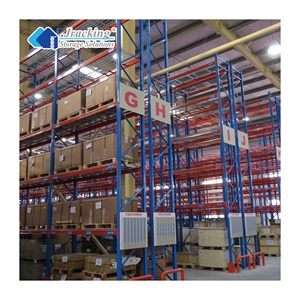
 CE Certified
Factory Direct Inventory
Industrial Storage & Warehouse Racking Products
Explore our CE certified, heavy-duty industrial shelving rack configurations designed for high load bearing capacity, seismic resistance, and maximum cubic space utilization.
CE Certified
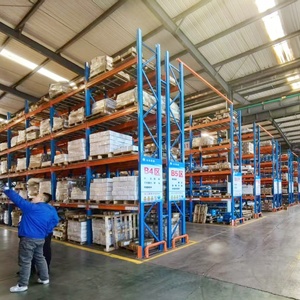 800-3000kg/Level
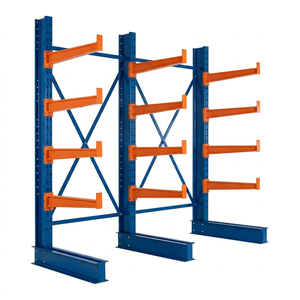 Heavy Tubing/Pipe
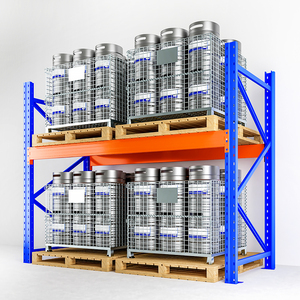 5000kg Capacity
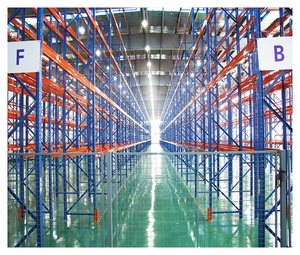 Box Beam Steel
 Workshop Grade
 5-Layer Multi-Level
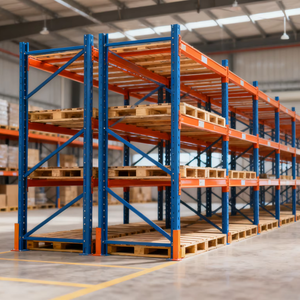 Powder Coated
Engineering Excellence: CE Certified Warehouse Racking Manufacturing
In modern supply chain architecture, structural storage integrity is the paramount factor governing operational efficiency, worker safety, and inventory optimization. As an established CE certified warehouse shelving racks factory and global supplier, our manufacturing paradigm centers on rigid engineering standards, high-yield cold-rolled steel metallurgy, and rigorous safety compliance including FEM 10.2.02 (European Handling Institute), ANSI MH16.1 (Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks), and ISO 9001 quality frameworks.
High-Grade Raw Steel Selection
We utilize prime cold-rolled steel (Q235B and Q355B structural grades) possessing superior yield points, high tensile elasticity, and uniform gauge consistency for all upright profiles and roll-formed box beams.
Precision Robotic Welding
Connector claws and heavy beam end-plates undergo automated pulse MIG welding. Penetration depth is monitored to eliminate shear stress vulnerabilities at load-critical junction points.
Electrostatic Epoxy Coating
Our automated multi-stage washing and electrostatic thermosetting epoxy powder coating line guarantees high chemical resistance, scratch immunity, and long-term anti-corrosion performance (ASTM B117 salt spray compliant).
Structural Dynamics & Seismic Design Considerations
Warehouse structural failure rarely originates from a single localized overload; rather, it manifests through cumulative structural fatigue, uncalculated eccentric loads, or insufficient seismic base anchoring. Modern industrial facilities operating under nearshoring pressure require custom structural engineering that factors in local ground acceleration, slab shear strength, and aisle safety clearances.
Every racking assembly supplied by our factory undergoes Finite Element Analysis (FEA) strain modeling prior to cold-forming production. Our structural engineers verify upright column profiles (featuring 80mm to 120mm face widths with multi-ribbed side geometry) to guarantee dynamic load stability up to 5,000 kg per bay level while restricting maximum beam deflection below L/200 of clear span span lengths.
Strategic Market Intelligence
Future Procurement Trends in Industrial Warehouse Storage (2025–2030)
Analyzing macro-economic shifts, automated material handling demands, and sustainability mandates transforming global warehouse procurement strategy.
1. Nearshoring & Rapid-Deployment Modular Systems
The global realignment of manufacturing hubs across North America, Europe, and Southeast Asia has catalyzed demand for quick-deploy, highly standardized selective racking infrastructure. Enterprise procurement officers are shifting away from rigid fixed-rack structures toward boltless, adjustable, modular rack frameworks that can be reconfigured in pitch increments of 50mm or 75mm as SKU profiles evolve.
2. Integration Readiness for Automation (AS/RS & AMR)
Traditional static storage is rapidly merging with semi-automated and fully automated material handling systems. Modern B2B procurement mandates that structural pallet racking accommodate automated guided vehicles (AGVs), Autonomous Mobile Robots (AMRs), and Radio Shuttle systems. This requires tighter manufacturing tolerances (+/- 1.0mm upright alignment), specialized guide rail channels, and floor-anchored safety barriers.
3. Total Cost of Ownership (TCO) vs. Initial CAPEX
Savvy logistics buyers look beyond initial metric-ton steel purchasing price. Long-term operational audits demonstrate that rack systems engineered with reinforced column bases, heavy-duty structural row spacers, and wire mesh decking yield a 65% reduction in annual maintenance downtime caused by forklift impacts. TCO-focused procurement prioritizes durability and audit compliance.
Engineering Specification Benchmark
Heavy-Duty Warehouse Shelving & Racking Comparison Matrix
Standardized structural properties and application benchmarks across major industrial storage configurations.
| Racking System Type | Primary Load Profile | Standard Load Capacity | Structural Steel Grade | Selectivity vs Density | CE & EN Compliance |
|---|---|---|---|---|---|
| Heavy-Duty Selective Pallet Rack | Palletized Goods / Multi-SKU | 1,000 kg – 4,000 kg / Level | Q235B / Q355B Cold-Rolled | 100% Selectivity / Moderate Density | FEM 10.2.02 / EN 15512 |
| Industrial Cantilever Racking | Pipes, Tubing, Timber, Steel Bar | 500 kg – 1,500 kg / Arm | Structural H-Beam / Hot-Rolled | Direct Crane/Forklift Pick Access | EN 1090-1 / CE Certified |
| High-Density Drive-In Racking | Homogeneous Bulk SKU Loads | 1,000 kg – 1,500 kg / Pallet | Cold-Formed High Tensile Steel | Low Selectivity / Max Cubic Density | ANSI MH16.1 / CE Certified |
| Radio Shuttle Automation Rack | Deep-Lane High Volume Storage | 1,500 kg / Pallet Position | Precision Cold-Rolled Channel Steel | Semi-Automated LIFO / FIFO | ISO 9001 / CE Certified |
| Multi-Tier Shelving Mezzanine | Cartons, Small Parts, Manual Pick | 300 kg – 800 kg / Floor m² | Perforated Upright Profile | High Manual Access Efficiency | EN 15635 Safety Standard |
Innovation Roadmap
Technological & Structural Development Trends in Warehouse Racking
How material science, surface protection engineering, and smart monitoring are shaping next-generation industrial shelving units.
Advanced High-Yield Cold-Formed Steel Profiles
Steel metallurgy breakthroughs allow factories to utilize thinner-gauge, high-tensile steel alloys (such as micro-alloyed Q355B steel) that deliver equivalent or superior beam moment of inertia while reducing structural tare weight. This allows multi-tier mezzanine and high-bay racking systems to achieve higher loading thresholds without placing excessive stress on floor slab foundations.
Eco-Friendly Thermosetting Surface Treatments
Environmental regulations governing volatile organic compounds (VOCs) have accelerated the adoption of zero-emission powder coating lines. Our factory incorporates 99% paint-recovery electrostatic coating systems utilizing lead-free epoxy resins that withstand severe thermal fluctuations in cold-storage environments (-30°C) without micro-cracks or delamination.
Direct Factory Advantage
Why Global Enterprises Partner With Our Manufacturing Facility
From OEM/ODM structural customization to full supply chain transparency and seismic design verification.
Full In-House Roll-Forming
Operating over 20 continuous automated roll-forming lines for beam and upright manufacturing, ensuring consistent geometry, precise pitch punching, and tight dimensional tolerance.
Stringent Quality Assurance
Every steel batch is tested for yield strength, elongation, and chemical composition. Finished products undergo regular destruction testing and weld joint ultrasonic inspection.
Global Regulatory Compliance
Fully certified for international export with CE Mark documentation, ISO 9001:2015, ISO 14001:2015, and compliance verification for North American and European logistics standards.
Technical Procurement Knowledgebase
Frequently Asked Questions (FAQ) - Warehouse Racks Procurement
Expert answers to critical engineering, regulatory compliance, and installation questions asked by logistics buyers.
What certifications should a reputable warehouse shelving rack supplier possess for global export?
A qualified industrial racking manufacturer must hold CE Certification (conforming to EN 1090-1 / EN 15512 structural steel requirements), ISO 9001 Quality Management Certification, and ISO 14001 Environmental Management Certification. For projects in North America, compliance with RMI (Rack Manufacturers Institute) and ANSI MH16.1 standard guidelines is essential for passing local building code inspections and insurer safety audits.
How do you calculate load capacity and structural safety factors for heavy-duty pallet racks?
Load capacity is calculated based on uniformly distributed load (UDL) principles, factoring in beam length, cross-sectional inertia, upright frame height, unbraced length, and vertical bay spacing. Structural calculations incorporate a standard safety factor between 1.5 and 1.8 per FEM 10.2.02 guidelines. Beam deflection is engineered not to exceed L/200 under full rated load to prevent permanent plastic deformation.
What is the difference between cold-rolled box beams and step beams in pallet racking?
Cold-rolled box beams consist of two C-sections interlocking to form a enclosed rectangular tube, offering superior torsional rigidity and heavy load bearing capacity suitable for heavy pallets. Step beams feature an internal L-shaped step along the top edge, designed specifically to retain wire mesh decking, steel panels, or drop-in support bars flush with the top of the beam.
How are racking systems engineered for high-risk seismic zones?
Seismic-resistant racking design incorporates enlarged base plates, heavy-duty wedge or chemical floor anchors, augmented diagonal frame bracing, and higher yield steel grades. Structural engineers evaluate the site ground acceleration coefficient (Z-factor) and building slab thickness to prevent rack sway, shear anchor failure, or frame collapse during seismic events.
When should a warehouse choose Cantilever Racks over Pallet Racks?
Cantilever racking is specifically engineered for long, bulky, or irregular linear materials such as steel pipes, PVC tubing, timber planks, aluminum extrusions, and sheet metal. Unlike pallet racking, cantilever systems feature unobstructed front aisles without front vertical columns, enabling continuous horizontal storage and easy overhead crane handling.
What surface protection option is best for cold storage or outdoor environments?
For dry ambient indoor warehouses, high-grade electrostatic epoxy powder coating provides excellent durability and aesthetic color-coding. However, for outdoor yards, high-humidity processing facilities, or sub-zero cold storage operations, Hot-Dip Galvanizing (HDG) per ISO 1461 is strongly recommended as it creates a thick zinc-alloy metallurgical barrier that prevents rust even if the surface is scratched.
Optimize Your Warehouse Storage Capacity & Safety
Connect directly with our engineering team for free CAD warehouse layout designs, structural load calculations, and competitive direct factory pricing on CE certified racking systems.